


PE100 Socket Fusion Fittings - dn20 to dn63, SDR11
Small-bore PE100 work is decided in the fitting, not in the pipe. Once the pipe run is dn63 or below, a butt fusion machine is the wrong tool on a congested site: it needs a perfectly straight run of both ends at exactly the right height, and it needs that alignment twice. A socket fitting asks for none of it. The pipe is cut, squared, chamfered, pushed into a tapered socket and fused in place, so the joint can be made in a trench, in a chamber, or on a live service where the two pipes never line up. Everything on this page belongs to that way of working.
The term worth fixing first, because it is used loosely in the trade: 热熔承插 is socket fusion, and it is not the same process as electrofusion. To answer what is socket fusion in one line - the pipe end and the inside of the socket are heated together, usually by a hot plate or a hot air gun, and the pipe is pushed into the socket while the polymer is molten. The joint is made by the pipe material and the fitting material flowing into each other. There is no resistor wire inside the socket, no control unit clamped over terminals and no barcode-driven cycle. That distinction is not academic: a socket fusion fitting and an electrofusion fitting can sit in the same catalogue, look similar in a photograph and require completely different tooling on site.
The range below is a single wall series. Every size from dn20 to dn63 is SDR11, which for PE100 resin corresponds to PN16. That is a deliberate restriction on this page rather than a gap in the range: small-bore service connections are the one place where a thicker wall earns its cost, because the fitting is small enough that the socket, not the pipe, is the weakest point in the assembly.

Section 1 of the drawing set. Every value on the drawing is reproduced in the dimension schedule below.
What the thirteen fitting families cover
The catalogue behind this page is organised the way the parts actually arrive on site: by the job the fitting has to do, not by the shape it happens to be moulded in. Nine of the thirteen families are plain socket fittings, where both ends are the same fusion socket and the fitting does one thing - join two pipes, step one diameter down, split a run, turn a corner or close an end. The remaining six are threaded transitions, where one end is a fusion socket and the other is a metal or plastic thread, and those are the fittings that tie a PE100 run to a meter, a valve, a regulator or an existing galvanised line.
The nine all-socket families
Search hdpe socket fusion fittings in any catalogue and you will get a list that mixes socket fittings, butt fusion fittings and threaded fittings under one heading, which is why buying from a general list often ends with the wrong part in the carton. On this page the socket fitting is precisely the fitting whose socket carries its own heater, and every schedule below belongs to that definition. That distinction matters most on small bore, where a dn63 socket and a dn63 butt-fusion end look almost identical in a photograph and require completely different tooling and a completely different joint.
Straight-through work is covered by the socket coupling - search hdpe socket fusion coupler and it is the part that comes back - which joins two pipes of the same diameter and is the fitting that appears most often in a bill of materials, usually in pairs, because a length of pipe between two devices needs a coupling at each end. Diameter changes are covered by the socket reducer, which comes in fifteen size combinations and is the largest single table on this page. Branching is covered by two tees, a straight tee for a symmetrical split and a reducing tee where the branch is smaller than the run. Direction changes are covered by the 45 degree and the 90 degree elbow. End closure is covered by the socket plug.
The six threaded transitions
A socket fusion gas pipe run is assembled almost entirely from this page, because a gas service line ends at a threaded port more often than at another PE length. The other end of a threaded transition is rarely PE100, and that is the point of the fitting. A male thread adaptor hdpe part is the standard way to leave a PE100 run and pick up a metal system, and the range of ports it has to meet is wide: meters, regulators, valves, flanges, irrigation controllers and legacy galvanised risers. Six families cover the combinations that occur: male and female threaded couplings, male and female threaded 90 degree elbows, and male and female threaded tees. The male version screws into a female port; the female version is what you fit when the port is male. Getting this the wrong way round is the single most common ordering error in this family, so the thread gender is spelled out in the part number rather than left to the reader.
Where the table stops
Buyers usually reach this page through a generic search for fittings for hdpe pipe and then have to work out which of the many fitting types on the market they actually need. The short version is that hdpe pipe connection fittings divide into three families by how the joint is made - butt fusion, socket fusion and mechanical - and this page covers one of those three, the socket fusion family, in the small-bore band. If your project is in dn90 and above, you are looking at a different schedule. The size limit here is not a manufacturing preference. Above dn63 the economics change: the fittings become larger than the pipes they connect, the moulding tool cost rises sharply, and the socket fusion process starts to compete with butt fusion, which is the method used for the dn90 and above socket fusion fittings. If a project mixes dn63 and dn90 in the same run, plan the transition deliberately at the dn63 end rather than expecting one fitting to bridge it.
| No. | Fitting | What it does to the run | Sizes published | SDR |
|---|---|---|---|---|
| 1 | Socket Fusion Coupling 热熔承插直接 |
Joins two pipes of the same diameter | 6 | 11 |
| 2 | Socket Fusion Reducer 热熔承插异径直接 |
Steps the diameter down in a straight run | 15 | 11 |
| 3 | Socket Fusion Tee 热熔承插三通 |
Splits one run into two | 6 | 11 |
| 4 | Socket Fusion Reducing Tee 热熔承插异径三通 |
Splits one run into two | 15 | 11 |
| 5 | Socket Fusion 45 Degree Elbow 热熔承插45°弯头 |
Changes direction without leaving the trench | 6 | 11 |
| 6 | Socket Fusion 90 Degree Elbow 热熔承插90°弯头 |
Changes direction without leaving the trench | 6 | 11 |
| 7 | Socket Fusion End Cap 热熔承插管堵 |
Closes an end or a future branch point | 6 | 11 |
| 8 | Socket Fusion Female Threaded Coupling 热熔承插内螺纹直接 |
Ends a PE100 run at a metal or plastic thread | 6 | 11 |
| 9 | Socket Fusion Male Threaded Coupling 热熔承插外螺纹直接 |
Ends a PE100 run at a metal or plastic thread | 6 | 11 |
| 10 | Socket Fusion Female Threaded 90 Degree Elbow 热熔承插内螺纹90°弯头 |
Ends a PE100 run at a metal or plastic thread | 6 | 11 |
| 11 | Socket Fusion Male Threaded 90 Degree Elbow 热熔承插外螺纹90°弯头 |
Ends a PE100 run at a metal or plastic thread | 6 | 11 |
| 12 | Socket Fusion Female Threaded Tee 热熔承插内螺纹三通 |
Ends a PE100 run at a metal or plastic thread | 6 | 11 |
| 13 | Socket Fusion Male Threaded Tee 热熔承插外螺纹三通 |
Ends a PE100 run at a metal or plastic thread | 6 | 11 |
How the socket is heated
There are two heat sources in service for small-bore PE100 and the choice between them is a site decision, not a product decision. A hot plate is a thermostatically controlled metal block with a socket-shaped recess milled into it; the fitting is pressed into the recess, heated for a set time, then removed and the pipe pushed straight in. A hot air gun blows heated air around the outside of the socket while the pipe end is simultaneously heated in the same stream. The hot plate gives a more even and more repeatable result; the hot air gun reaches awkward shapes and confined positions where a plate will not seat. Either way, the heat arrives from outside the fitting, and both surfaces reach fusion temperature at the same moment.
Why both surfaces have to reach melt together
The joint is made by the pipe and the fitting flowing into each other, so it fails if one side is ahead of the other. Push a cold pipe into a hot socket and the pipe end softens before it is deformed, so it does not expand to fill the taper and the joint has a dry region at the root. Heat both sides equally and the two materials interpenetrate and cool as one body, which is why the heating step in a socket fusion joint is specified in seconds and not in degrees, and why the rule of thumb is that a hotter plate left longer will make a weak fitting and a colder plate left longer will make a fitting that never flows at all. The window is narrower than people expect, and the cure for a joint that will not go together is a re-cut end, not more heat.
Socket fusion and electrofusion compared
Search socket fusion vs electrofusion and the results mix the two freely, usually because both end in the word fusion. Plastic pipe socket fusion as a process term therefore covers two quite different things, and the practical comparison is worth making explicitly. In electrofusion the fitting carries a resistor wire moulded into it and the heat is generated inside the socket by current; the control unit measures the wire resistance, runs a preheat and a main cycle, and aborts if the resistance drifts. In socket fusion there is no element and no controller; the heat comes from the plate or the gun, and the technician controls the result by time and by temperature at the plate. The consequences run through everything downstream. An electrofusion fitting is single-use, because the melted polymer cannot be recovered. A socket fusion fitting is equally single-use, because the socket has been re-melted and will not take a second pipe soundly - but it is re-usable as a cold fitting if the heat is stopped short. And a socket fusion joint can be made on a pipe that is not aligned, in a confined space, with one person and a hot plate, which is why the process dominates small-bore service work.
What a good socket looks like after the push
A correctly made socket fusion joint shows a small, continuous bead of extruded material at the mouth of the socket, all the way round, sitting proud of the fitting face. That bead is the only visual evidence that the socket was filled to the root, and its absence on one side of the joint means the pipe was not pushed far enough or was not fully melted before it was seated. The bead should be even in height rather than heavier on one side, which is what distinguishes a joint that went in square from one that went in while it was still soft and skewed. The fitting is then left undisturbed to cool; the bead is fully strong only when cold, and pulling the assembly straight off a hot plate and twisting it deforms the socket before it has stabilised.
Pipe preparation before the fitting goes on
The joint quality is decided before the machine is switched on. Four things have to be right, and they are checked in this order every time: the pipe is the right grade and series, the end is square, the end is clean, and the end is chamfered. A pipe that is PE80 or a different SDR will fuse to a fitting perfectly well mechanically and still be wrong on paper, so the marking is read before anything is cut.
Squaring and reaming
The cut has to be square because the socket is tapered and a square end gives a uniform melt band all round. In practice a square end is achieved by rotating the pipe in a vice-clamped pipe cutter and taking several turns rather than one, then reaming the internal burr with a round file or a reamer. The burr matters more than it looks: an internal bead of extruded material left on the end of the pipe will sit inside the fusion zone and can become the initiation point for a leak path. Sawing with a hand saw leaves an oval end and is not acceptable for a pressure joint.
Chamfer and insertion depth
The chamfer is what allows the pipe to enter the socket at all. A pipe end turned square to the axis has an outside edge that fouls the taper, so it has to be relieved at roughly 30 to 45 degrees over 2 to 3 mm, until the pipe enters by hand with the weight of the pipe behind it and no force. The insertion depth is marked on the pipe with a witness line. The reference figure used on this page is 12 mm at dn20 rising to 38 mm at dn63, which is 0.6 x dn rounded to the millimetre. Treat that as a site reference rather than a catalogue dimension, and follow the depth printed on the fitting itself where the two differ.
Cleaning and the storage of prepared ends
Fusion quality falls off sharply if the pipe end has been touched. The end is wiped with a lint-free cloth, and it is not put down in mud, stepped on or handled again between prep and fusion. The same rule applies to the inside of the socket: a socket that has had its liner scratched by a previous fitment attempt is a socket that will not fuse evenly. Prepared ends are stored capped, and they are used the same day. Where a run has to be left open overnight, the pipes are capped rather than left open, because an open PE100 pipe collects water and debris that end up in the fusion zone.
| DN | Reference insertion depth (mm) | How it is marked on site |
|---|---|---|
| dn20 | 12 | Witness line 12 mm from the cut end |
| dn25 | 15 | Witness line 15 mm from the cut end |
| dn32 | 19 | Witness line 19 mm from the cut end |
| dn40 | 24 | Witness line 24 mm from the cut end |
| dn50 | 30 | Witness line 30 mm from the cut end |
| dn63 | 38 | Witness line 38 mm from the cut end |
How a joint is made and checked
The sequence itself is short, and the discipline is in not shortening it. The plate is brought to temperature and the fitting is set into it and left for the specified heating time. The pipe end is then brought in axially, and the push is made in one movement - the pipe is seated fully to the witness mark and held there without twisting, because twisting after the push is the commonest cause of a joint that leaks at the root. The assembly is then left undisturbed, off the plate, until it has cooled, and only then is it handled or buried.
Cooling and handling
The bead that forms around the joint at the mouth of the socket is the visible evidence that the socket was filled, and it is at full strength only after cooling. Pulling the assembly straight off the plate and twisting it, or supporting it in a way that loads the still-warm socket, distorts the joint before it has stabilised. In hot weather the cooling allowance is longer, and the filler material under the pipe is worth using on a hot day because it removes the support from the fitting while the polymer is still soft.
How the joint is verified
Two checks are applied on site, and a third in the laboratory. The visual check is the fusion bead: it should be continuous and of even height all round the socket mouth, and a bead that is present on one side only points to an incomplete push or a skewed assembly. The second check is the witness line: if the pipe was marked to the correct insertion depth before the push and that line is now flush with the fitting face, the socket was filled to the root. Fusion joint strength and dimensional checks are carried out in our own CNAS-accredited laboratory and reported per batch on request, which is what turns a process argument into a specification item.

Socket fittings in this size band are injection moulded, one cavity per shot.
Connecting PE100 to metal and plastic
Every small-bore PE100 installation ends at a threaded port, and this is where most of the range is actually consumed. A typical meter station is built from four threaded fittings and a length of PE100 pipe: a male threaded coupling to leave the PE side, a male threaded elbow to turn towards the meter, a female threaded coupling to come back to PE, and a tee where a test point is required. The rest of the page is the schedule for those six families.
Thread form and sealing
The metal thread on these transitions is a standard gas thread, and the seal is made at the thread, not at a separate face. The female thread carries an internal shoulder which is what the male thread bottoms against; this is the metal-to-metal seal and it must be clean and undamaged. No thread sealant tape or compound is used on a gas-pressure joint, because a sealant that behaves correctly on a low-pressure water union can extrude into the gas stream at pressure and it also makes the joint non-verifiable. On a threaded transition in a gas line, the correct sealing method is the thread itself, tightened to the specified torque with the fitting reaching its thread shoulder. Where a sealant is required by local practice, it must be a product approved for gas service and applied to the thread only.
Choosing between male and female
The rule is simple and it is decided by the port, not by the fitting. If the device has a male port, the fitting needs a female thread. If the device has a female port, the fitting needs a male thread. The naming on the fitting refers to the thread on the fitting itself, which is the opposite of what some buyers assume. When a bill of materials mixes PE100 to meter, PE100 to valve and PE100 to existing galvanised, the genders will usually differ, and the schedule below states them per part so that the ordering does not depend on memory.
Threaded transitions on potable water
The water material approval covers the moulded bodies used for contact with wholesome water up to 65 °C, and the threaded variants are supplied against the same approval. The metal thread component is a separate material in the assembly and is certified independently. Machined sizes fall outside the moulded approval scope, so the threaded families in this range are within scope and the machined large-biameter fittings are not the same approval.
Socket fusion fittings in photographs
The photographs below are of the fittings we stock rather than of a computer model, and they are laid out family by family so that a part on a bench can be matched to a line in the schedule that follows. The whole range is moulded from the same PE100 compound in the same SDR 11 wall series, so what changes from one photograph to the next is geometry: how many socket mouths there are, which way they face, whether the run steps down, and whether a metal thread has been moulded into the body instead of a socket. Those are differences the eye catches immediately and a size list does not show at all.
Eleven of the thirteen families are photographed here. The two threaded elbows have not been photographed, and their places are left open rather than filled with a picture of the nearest similar part, because a threaded elbow on a plain elbow body is not the same component. Sizes and the wall series for both are in the schedule below, and photographs can be supplied on request. Where a body is clearer from more than one angle, every useful angle is shown, since the difference between a forty-five and a ninety is easier to see than to describe. The parts are shown as moulded and unpainted, so the surface in the photographs is the surface that arrives.


 7. Socket Fusion End Cap


 12. Socket Fusion Female Threaded Tee

Size schedules by fitting family
The schedules below reproduce the published sizes for this range exactly as they are held in the product list. Every entry is SDR11. There is no SDR17 line in this range and no second column of series, which is the single most useful thing to know before you order: the SDR is not a variable here, so a schedule read off a larger-diameter catalogue will not apply.
How to read a reduction size
A reduction is written large bore first, and the two numbers are the two pipe diameters it joins, not a length and a diameter. dn25×20 is a fitting that takes dn25 pipe on one side and dn20 on the other, and it is the transition between a dn25 run and a dn20 branch. The schedule lists the available combinations rather than every mathematically possible pair, so a combination that is not listed is not a combination that is moulded. Where a reducing tee is used, the run and the branch are marked in the same way, and the three listed reductions on the tee tables follow the same rule.
Threaded sizes and the inch side
The elbow families are where the thread gender changes the shape of the run, and it is worth deciding that before ordering rather than on site. An hdpe 90 degree elbow exists in three distinct forms: the plain all-socket version, which turns a PE100 run through ninety degrees, and the male and female threaded versions, which turn a PE100 run into a metal system at ninety degrees. Those are three different parts doing three different jobs, and the schedules below list all three separately rather than merging them under one elbow heading. A threaded size is written as two diameters as well, but the second number is an inch figure rather than another DN value. The dn side takes PE100 pipe by socket fusion and the inch side takes the metal or plastic thread. Note that some sizes carry a compound dimension such as dn40×1(1/4)寸, where the fitting offers a one-inch thread and a quarter-inch variant from the same body; both are listed as separate entries in the schedule and both are orderable. The inch figures are BSP, and they are not interchangeable with NPT, which has a different thread angle and a different pitch.
Straight-through parts and end closure
1. 热熔承插直接
Socket Fusion Coupling
dn20SDR 11dn25SDR 11dn32SDR 11dn40SDR 11dn50SDR 11dn63SDR 11
7. 热熔承插管堵
Socket Fusion End Cap
dn20SDR 11dn25SDR 11dn32SDR 11dn40SDR 11dn50SDR 11dn63SDR 11

| Company | Zhejiang Qingfa Pipe Technology Co., Ltd. |
| Business | PE100 / PE80 gas and water pipe, butt fusion and socket fusion fittings |
| Works address | No. 288, Da'an Road, Jiande, Hangzhou, Zhejiang, China |
| Website | www.qingfaindustry.com |
Reductions, 15 available combinations
| Size | Wall series | ||||||||||||||||||||||||||||||||||
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
|
|
Branches
| Size | Wall series | Branches |
|---|---|---|
| dn20 | SDR 11 | equal |
| dn25 | SDR 11 | equal |
| dn32 | SDR 11 | equal |
| dn40 | SDR 11 | equal |
| dn50 | SDR 11 | equal |
| dn63 | SDR 11 | equal |
| Run | dn25 run → dn20 branch | dn32 run → dn20 branch | dn32 run → dn25 branch | dn40 run → dn20 branch | dn40 run → dn25 branch | dn40 run → dn32 branch | dn50 run → dn20 branch | dn50 run → dn25 branch | dn50 run → dn32 branch | dn50 run → dn40 branch | dn63 run → dn20 branch | dn63 run → dn25 branch | dn63 run → dn32 branch | dn63 run → dn40 branch | dn63 run → dn50 branch |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| dn25 | dn32 | dn40 | dn50 | dn63 | |||||||||||
| 20 | |||||||||||||||
| 20 | 25 | ||||||||||||||
| 20 | 25 | 32 | |||||||||||||
| 20 | 25 | 32 | 40 | ||||||||||||
| 20 | 25 | 32 | 40 | 50 |
Direction changes
Dimension drawing and what each measurement controls
The drawing below is section 1 of the fitting dimension set, covering the socket fusion coupling from dn20 to dn63. It is reproduced here because the size schedule elsewhere on this page only carries the diameter and the wall series, and a schedule alone is not enough to set out a run: the socket is tapered, so the length of the insertion has to come from somewhere, and the six dimensions below are what fix it. Every value is taken directly off the drawing, with the tolerance the drawing states for each.
Reading the four diameters
Four diameters appear on the drawing and they are not interchangeable. D1 and D4 are the outside diameters of the body, D1 at one end and D4 at the other, and they are not equal because the body is drafted to clear the socket bore. D2 and D3 are the socket itself: D2 is the bore at the mouth, which is the opening the pipe has to enter, and D3 is the bore deeper in, where the wall of the fitting is thickest and where the melt has to reach to fill the root of the joint. The gap between D2 and D3 is the taper of the socket, and it is what makes a cold dry fit possible during assembly and a gas-tight joint once the pipe is pushed home. Anyone checking a fitment against a drawing should measure the socket, not the outside.
The two lengths and what they are used for
L1 is the insertion depth at each end: the distance the pipe has to enter the socket for the joint to be filled to the root, and it is the number a fitter marks on the pipe before the push. L is the overall length of the fitting from face to face, and it is the number that matters when the fitting is set out between two fixed points, because L1 is counted twice once the pipe is seated. Search hdpe 90 degree elbow dimensions in a supplier catalogue and this distinction is the one that gets lost, because catalogues often print the overall length as the single dimension and leave the insertion depth to be inferred from the drawing. The same convention applies to the 45 degree elbow, the tee and the reducer on this page, with the socket depth taken from the corresponding section of the drawing set.
Why the tolerances are asymmetric
The drawing states a different tolerance on each column, and the pattern is deliberate. D2 and D3, the two socket bores, are held to a few tenths of a millimetre because they are the surfaces that decide how tightly the pipe is gripped and how much melt is available at the root. The body diameters D1 and D4 are looser, and D4 looser still, because they carry no pressure and nothing is measured against them on site. The lengths sit between the two: L1 is held to a millimetre because it is transferred to the pipe as a witness line, and L is looser because it is a layout dimension. The practical consequence is that a socket which measures inside tolerance but is slightly oversize will feel tight and a slightly undersize one will feel loose, which is a useful check before the plate is switched on.
| Size | D1 +/-0.2 |
D2 +/-0.2 |
D3 +/-0.3 |
D4 +/-1 |
L1 +/-1 |
L +/-2 |
|---|---|---|---|---|---|---|
| dn20 | 19.4 | 19.2 | 17 | 27 | 15 | 32 |
| dn25 | 24.3 | 24.1 | 22 | 32 | 17 | 36 |
| dn32 | 31.3 | 31.1 | 29 | 40 | 19 | 40 |
| dn40 | 39.2 | 39.0 | 37 | 48 | 22 | 47 |
| dn50 | 49.1 | 48.9 | 47 | 60 | 25 | 54 |
| dn63 | 62.2 | 61.9 | 59 | 76 | 29 | 62 |
| Tolerance | +/-0.2 | +/-0.2 | +/-0.3 | +/-1 | +/-1 | +/-2 |
Ordering, packing and supply
The range is small enough to be stocked rather than made to order, and that is deliberate: the fittings on this page are used on repair work and on meter stations, where the job waits for the part. Cartons are labelled with the fitting family, the size and the SDR series, and the label is the same label used to pick the part in the warehouse. Private-label orders replace the factory branding on the body, the carton and the pallet, so the artwork and the mould identification are agreed before the first shot rather than added afterwards.
What arrives on a pallet
Socket fittings are small and nest or box efficiently, so a mixed pallet of this family carries a high piece count. The size marking is moulded into the body and is legible on the part itself rather than on a label, which is what lets a fitter confirm the size at the trench after the carton has been opened and the parts shuffled. Pallets are labelled with the purchase order, the item breakdown and the SDR series, and the same marking appears on the carton so that a pallet broken down at site still carries its identification.
Supplying against a small-bore project
For a project rather than a single fitting, the useful question is which of the thirteen families the design actually needs and in what quantity, because the threaded six and the socket seven have different order lead times and different shelf lives. State the medium, because the certificate that travels with the batch is chosen by the medium: gas-grade fittings can carry yellow marking and are supplied against the gas standards, potable water fittings against the water standards, and the two are not interchangeable on paperwork even though the body is the same.

Cartons are labelled by fitting type, size and SDR series.
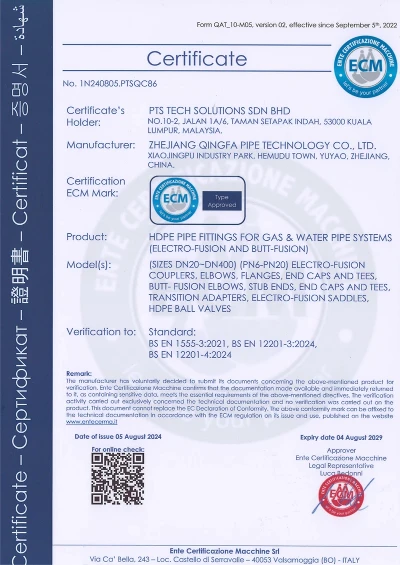
Certification documents


Questions we are asked about this range
-
![PE100 Socket Fusion 45 Degree Elbow, Dn63]() PE100 Socket Fusion 45 Degree Elbow, Dn63
PE100 socket fusion 45 degree elbow in SDR11, dn20 to dn63. Two sockets at 135 degrees give a shallow turn with low head loss. ECM and WRAS approved HDPE elbow.
-
![PE100 Socket Fusion Tee, Equal, SDR11]() PE100 Socket Fusion Tee, Equal, SDR11
Equal PE100 socket fusion tee in SDR11, dn20 to dn63. Three same-size socket mouths so a run branches without a reducer. ECM and WRAS approved PE100 fitting.
-
![HDPE Socket Fusion Reducer]() HDPE Socket Fusion Reducer
HDPE socket fusion reducer in SDR11, 15 pairs from dn25x20 to dn63x50 in one body. A reducing coupling with no separate step. ECM and WRAS
-
![PE100 Socket Fusion Coupling, SDR11]() PE100 Socket Fusion Coupling, SDR11
PE100 socket fusion coupling in SDR11, dn20 to dn63. An HDPE socket fusion fitting joining two plain pipe ends. ECM type approval, WRAS approved for gas.


