





Bend Steel To Plastic Transition Fitting PE Steel Riser
Pre-bent steel risers: the PE-to-steel joint that turns the corner
Where the steelwork has to leave the main at an angle, a straight transition forces the installer to weld an elbow immediately downstream of the PE joint. A bend steel to plastic transition fitting removes that weld: the 90° turn is formed in the steel leg in the factory, and the whole assembly arrives with one PE socket to fuse and one steel end to connect.
Qingfa supplies the PE steel bend transition in 34 size pairings from dn25 to dn110, in two overall steel leg lengths. It is the fitting utilities reach for when a poly gas pipe riser has to come up out of a trench against a wall, or when an existing service has to be picked up from a main that does not run in line with it. The same part is bought in the UK as a steel to HDPE transition fitting, and in the Gulf as a steel to PE transition fitting - the leg length and the DN pairing are what the order has to settle.
Choosing between the 1.1 m and 1.5 m steel leg
The two lengths exist for two different trench conditions, not as a size upgrade. The 0.3 m dimension is the straight portion before the bend on both versions; only the portion after the bend changes.
| Condition on site | Steel leg to order |
|---|---|
| Riser finishes below the meter box, short exposed run | 1.1 m (0.3 m + 0.8 m) |
| Meter box set high on a wall, or deep trench below the turn | 1.5 m (0.3 m + 1.2 m) |
| Second bend or offset needed after the transition | 1.5 m - leaves stock for the second bend |
| Confined chamber, minimal exposed steelwork wanted | 1.1 m |
Ordering the longer leg is the safer default when the final riser height is not fixed at order stage, because the leg can be cut back on site.
Bend geometry and head loss
A factory-formed bend in a steel leg of this length adds very little loss compared with a site-welded elbow of the same nominal size. The reason is internal finish: the pre-bent leg is formed from seamless tube with a controlled bend radius, so there is no weld bead projecting into the flow and no misalignment between two welded ends.
For gas distribution at the pressures these fittings normally see, the bend is not a significant pressure drop in the system - the meter and the service regulator are. Where the fitting does matter is in flow-induced vibration at the turn: a continuous leg is stiffer than a welded elbow and moves less under line pressure fluctuation.
The bend range at a glance
| Group | Size pairings in the group |
|---|---|
| SDR11 · threaded steel end available - 16 pairings | |
| PE socket dn25 → steel leg DN22 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn25 → steel leg DN27 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn32 → steel leg DN27 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn32 → steel leg DN34 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn40 → steel leg DN27 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn40 → steel leg DN34 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn40 → steel leg DN42 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn40 → steel leg DN48 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn50 → steel leg DN34 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn50 → steel leg DN42 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn50 → steel leg DN48 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn63 → steel leg DN34 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn63 → steel leg DN42 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn63 → steel leg DN48 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn63 → steel leg DN60 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn90 → steel leg DN89 | 1.1 m and 1.5 m overall steel leg |
| SDR11 · welded or flanged steel end only - 16 pairings | |
| PE socket dn32 → steel leg DN22 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn32 → steel leg DN32 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn40 → steel leg DN32 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn40 → steel leg DN38 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn40 → steel leg DN45 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn50 → steel leg DN32 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn50 → steel leg DN38 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn50 → steel leg DN45 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn50 → steel leg DN51 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn63 → steel leg DN32 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn63 → steel leg DN38 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn63 → steel leg DN45 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn63 → steel leg DN51 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn63 → steel leg DN57 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn63 → steel leg DN63 | 1.1 m and 1.5 m overall steel leg |
| PE socket dn110 → steel leg DN108 | 1.1 m and 1.5 m overall steel leg |
| SDR17 · threaded steel end available - 1 pairings | |
| PE socket dn90 → steel leg DN89 | 1.1 m and 1.5 m overall steel leg |
| SDR17 · welded or flanged steel end only - 1 pairings | |
| PE socket dn110 → steel leg DN108 | 1.1 m and 1.5 m overall steel leg |
34 size pairings, each available in two steel leg lengths - 1.1 m (0.3 m + 0.8 m) and 1.5 m (0.3 m + 1.2 m), giving 68 part numbers. Both lengths are pre-formed to a 90° bend with the same PE socket and steel DN as the straight range.
Site conditions the bend range is specified against
- Trench walls where the riser must come up close to the excavation face
- Reinstatement limits that leave no room for an on-site elbow weld
- Fusion-trained crews without coded welders on the same site
- Ground movement or settlement risk, where one continuous leg is preferred to two welded parts
- Retrofit connections where the new main does not follow the old service alignment
What is and is not included in a bend transition
A bend transition is supplied as one assembly: PE socket moulded onto a steel leg that is already bent to 90°. It is not supplied with a backing plate, a riser clamp or a transition to copper - those are separate items.
If your drawing shows the bend made from two welded lengths of pipe, that is a different part and will not have the same fatigue behaviour at the turn. Give us the steel DN, the PE dn, the wall series and the leg length and we will confirm the part number against the table.
Quality control on the bend and the bond
The bond is the same process as on the straight range: the PE socket is moulded onto the prepared steel leg while the polymer is molten, so the interlock forms over the whole inserted length. On a bend this matters more, because the joint sees bending as well as axial load.
The leg is bent before the socket goes on, so the socket sits on a straight, stress-relieved section - not on the bend. That keeps the fusion zone round and keeps the electrofusion current even around the coil.
Packing a bend so it arrives straight
A bend is an awkward shape to crate well. Legs are nested so the bends do not press on each other, and the PE ends are separated from steel by a divider - a steel end resting against a fusion surface will scratch it. Caps stay on until the fitting is fused.

Finished PE fittings warehoused and staged for shipment at the Qingfa works
Certification and batch records
Batch records for every bend transition cover the tube heat number, the bend set-up, the PE batch, the moulding run and the dimensional check. The laboratory that signs them off is accredited to ISO/IEC 17025:2017, so the reports stand up to third-party review.
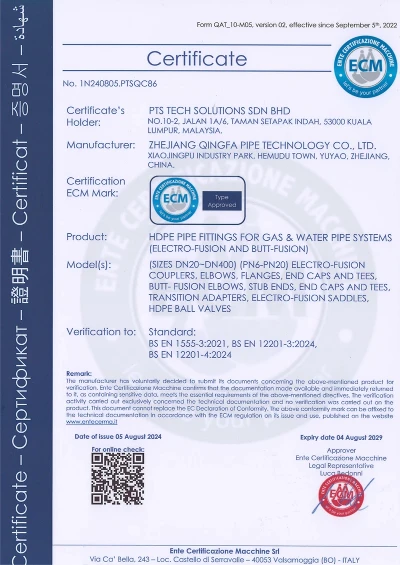
CE marking - ECM, dn20 to dn400
Issued by Ente Certificazione Macchine (ECM, Italy, notified body NB 1282). PE100 fittings for gas and water, dn20 to dn400, to BS EN 1555-3:2021 and BS EN 12201-3:2024.

CE - ECM voluntary attestation, dn20 to dn1200
ECM voluntary certification covering PE fittings dn20 to dn1200 to EN 12201-3:2024, EN 1555-3:2021 and Regulation (EU) No 305/2011.

CNAS laboratory accreditation - ISO/IEC 17025:2017
Accreditation of the Zhejiang Qingfa testing centre to ISO/IEC 17025:2017 under the CNAS-CL01 criteria.
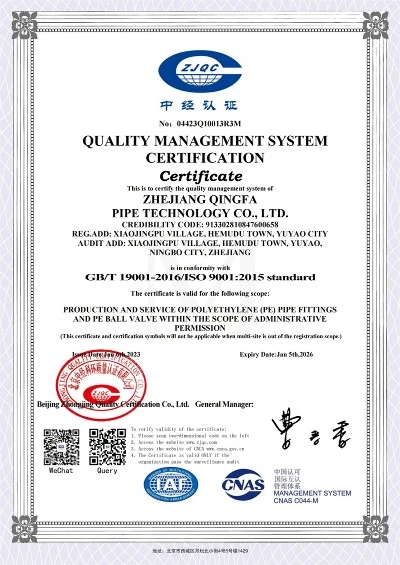
ISO 9001:2015 - quality management system
Quality management system for the production and service of PE pipe fittings and PE ball valves; issued by Zhongjing Certification.

ISO 14001:2015 - environmental management system
Environmental management system for the production and service of PE pipe fittings and PE ball valves; issued by China Economic Certification.

ISO 45001:2018 - occupational health and safety
Occupational health and safety management system for production and service activities; issued by Zhongjing Certification.

WRAS material approval
UK approval for material in contact with drinking water: PE100 black HDPE fittings to BS 6920-1:2014, for water up to 65 °C.

GB/T 27922-2011 - five-star after-sales service
After-sales service system of the HDPE pipe fittings range evaluated to the GB/T 27922-2011 commodity after-sales service standard at five-star level.
Common questions on pre-bent transitions
Can the steel leg be cut down on site?
Yes, on the steel end. The PE socket and the bend itself must not be altered, and the socket bore must stay capped until the moment of fusion.
Is the bend always 90 degrees?
The range is standardised on 90°. Other angles are made to order, and the lead time is longer because the bend form has to be set up. If the drawing shows an HDPE to steel transition at a shallower angle, send it and we will confirm what is feasible.
What is the minimum order quantity?
Orders can be mixed across sizes within the same leg length; a full carton per size is the practical minimum for an economic freight rate. Ask us for an MOQ against your actual size list.
Can the steel end be threaded on the bend range?
On the sizes marked in the table, yes - the group headings show which combinations carry a threaded option. The threaded sizes are the same steel to PE transition fittings as the welded ones, only the end finish differs.
Do you export the bend range, and can you quote CIF?
We manufacture in Zhejiang and export directly. Send the size list, leg length and destination port and we will quote FOB or CIF. Buyers comparing pre-bent riser fitting prices across PE steel transition suppliers can have a factory quotation the same working week.
Hot Tags: bend steel to plastic transition fitting pe steel riser, China bend steel to plastic transition fitting pe steel riser manufacturers, suppliers, factory
You Might Also Like


Send Inquiry