





Ductile Iron Threaded Steel To Plastic Transition Fitting
Ductile-iron threaded transitions for direct meter and service connections
At a meter or a service tee-off, the connection is almost never welded. It is threaded, and it has to be made up by hand in a pit with a wrench. A ductile iron threaded steel to plastic transition fitting exists for exactly that joint: the PE side fuses to the service pipe, and the iron side carries a taper thread that screws straight into the meter union or the existing steel tail.
Qingfa makes the ductile iron to HDPE transition fitting range in 14 size and thread combinations, dn25 to dn63. It is the smallest range in our steel-to-plastic family, and it is the one that gets fitted most often by hand rather than by machine.
Thread sizes available, dn25 to dn63
| Polyethylene end | dn25 electrofusion socket |
|---|---|
| Thread designation | R 3/4 |
| Pressure class basis | PE100, SDR11 |
| Outer body | ductile iron, machined |
| Polyethylene end | dn32 electrofusion socket |
|---|---|
| Thread designation | R 1 |
| Pressure class basis | PE100, SDR11 |
| Outer body | ductile iron, machined |
| Polyethylene end | dn32 electrofusion socket |
|---|---|
| Thread designation | R 3/4 |
| Pressure class basis | PE100, SDR11 |
| Outer body | ductile iron, machined |
| Polyethylene end | dn40 electrofusion socket |
|---|---|
| Thread designation | R 1 |
| Pressure class basis | PE100, SDR11 |
| Outer body | ductile iron, machined |
| Polyethylene end | dn40 electrofusion socket |
|---|---|
| Thread designation | R 1-1/4 |
| Pressure class basis | PE100, SDR11 |
| Outer body | ductile iron, machined |
| Polyethylene end | dn40 electrofusion socket |
|---|---|
| Thread designation | R 1-1/2 |
| Pressure class basis | PE100, SDR11 |
| Outer body | ductile iron, machined |
| Polyethylene end | dn50 electrofusion socket |
|---|---|
| Thread designation | R 1 |
| Pressure class basis | PE100, SDR11 |
| Outer body | ductile iron, machined |
| Polyethylene end | dn50 electrofusion socket |
|---|---|
| Thread designation | R 1-1/4 |
| Pressure class basis | PE100, SDR11 |
| Outer body | ductile iron, machined |
| Polyethylene end | dn50 electrofusion socket |
|---|---|
| Thread designation | R 1-1/2 |
| Pressure class basis | PE100, SDR11 |
| Outer body | ductile iron, machined |
| Polyethylene end | dn50 electrofusion socket |
|---|---|
| Thread designation | R 2 |
| Pressure class basis | PE100, SDR11 |
| Outer body | ductile iron, machined |
| Polyethylene end | dn63 electrofusion socket |
|---|---|
| Thread designation | R 1 |
| Pressure class basis | PE100, SDR11 |
| Outer body | ductile iron, machined |
| Polyethylene end | dn63 electrofusion socket |
|---|---|
| Thread designation | R 1-1/4 |
| Pressure class basis | PE100, SDR11 |
| Outer body | ductile iron, machined |
| Polyethylene end | dn63 electrofusion socket |
|---|---|
| Thread designation | R 1-1/2 |
| Pressure class basis | PE100, SDR11 |
| Outer body | ductile iron, machined |
| Polyethylene end | dn63 electrofusion socket |
|---|---|
| Thread designation | R 2 |
| Pressure class basis | PE100, SDR11 |
| Outer body | ductile iron, machined |
14 size and thread combinations, dn25 to dn63. R is the taper pipe thread series; the steel body is ductile iron rather than carbon steel because the thread is cut directly into it and has to take the make-up torque without cracking.
Why the thread is cut into ductile iron and not carbon steel
Carbon steel takes a thread well in thick wall, but at the wall thickness of a dn25 to dn63 service transition there is not much metal around a 2 inch taper thread, and a carbon steel thread in a damp pit will corrode at the crests - which is where a thread seals and where it grips. Ductile iron nodularises the graphite, so the material yields before it cracks and the thread takes make-up torque without chipping.
The practical consequence for the installer is simple: a wrench slipped on a ductile iron thread usually deforms it; on a carbon steel thread of the same size it often shears the crest off and the joint is scrap. On a fitting that will be made up in a street pit, that difference decides the material.
Sealing and make-up on a taper thread
The R series is a taper thread, so it seals by interference along the flanks as it is made up, not by seating on a face. Two consequences follow.
First, the thread is not meant to be bottomed out. It should engage the specified number of turns and then stop, with the seal made on the flanks. Forcing it further splits the boss rather than improving the seal.
Second, the sealant has to suit a taper joint. A thread tape or a jointing compound rated for gas service is applied to the male thread, and it must not be so thick that it changes the make-up depth, because that is what sets the engagement.
Matching the thread to what is already on the meter
The thread series in this range runs from 3/4 to 2 inch, matched to the PE size by what the service pipe actually has to carry. The pairing is not one-to-one: dn32 and dn40 each appear with several thread sizes, because the thread is chosen by the meter or the existing tail, not by the PE diameter alone.
If the existing connection is a different series - BSP parallel rather than taper, or a compression fitting rather than a threaded boss - say so at enquiry stage. Adapting a parallel thread to this fitting with a reducing bush is possible but the additional joint has to be allowed for.
In the UK and Ireland the PE side of this joint is usually supplied as an MDPE to steel adaptor, and the iron side as a set of ductile iron threaded fittings. The part is the same whichever name is on the enquiry; what differs is the thread standard the local meter uses, and that is the first thing to confirm before an order is placed.
Material of the PE side and the iron side
- PE side - PE100 socket, SDR11, with an embedded electrofusion coil, fused to the service pipe with a standard control box.
- Iron side - ductile iron body with a machined taper thread, sized to the R series in the table.
- Joint - the PE is moulded onto the prepared iron insert, forming a mechanical interlock over the full inserted length.
Where these fittings are made
Moulding, coil winding, iron machining and assembly happen on one site in Yuyao, so the iron body and the PE socket that have to fit together are produced under one quality system rather than bought in from separate suppliers and matched afterwards.

The raw-material feed that supplies every moulding press on site.

The moulding floor where the dn25 to dn63 PE sockets for the threaded range are produced.

A moulding press running the smaller socket moulds used across the threaded range.

Heavy press for the larger sockets, kept on the same site as the iron machining.

Winding the electrofusion coil that goes into each socket before moulding.

CNC machining of the ductile iron bodies and cutting of the taper threads.
Approvals and traceability for the threaded range
The threaded range is covered by the same CE marking, management-system certificates and laboratory accreditation as the rest of the PE100 fitting production. Certificates are issued with the batch, and the fusion test report for the run is available on request.
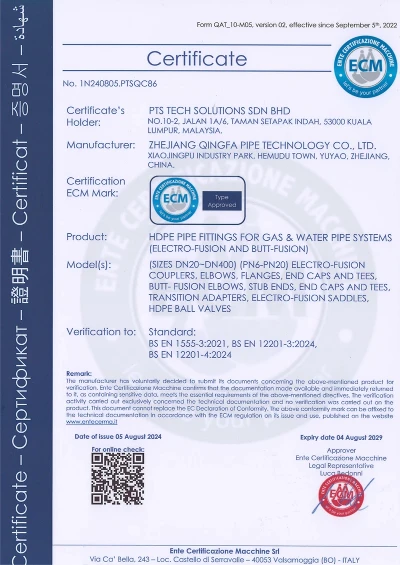
CE marking - ECM, dn20 to dn400
Issued by Ente Certificazione Macchine (ECM, Italy, notified body NB 1282). PE100 fittings for gas and water, dn20 to dn400, to BS EN 1555-3:2021 and BS EN 12201-3:2024.

CE - ECM voluntary attestation, dn20 to dn1200
ECM voluntary certification covering PE fittings dn20 to dn1200 to EN 12201-3:2024, EN 1555-3:2021 and Regulation (EU) No 305/2011.

CNAS laboratory accreditation - ISO/IEC 17025:2017
Accreditation of the Zhejiang Qingfa testing centre to ISO/IEC 17025:2017 under the CNAS-CL01 criteria.
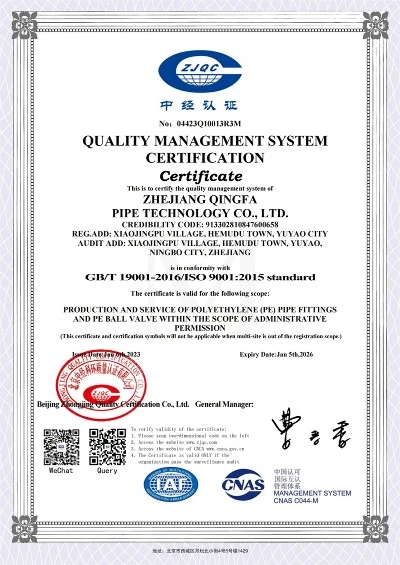
ISO 9001:2015 - quality management system
Quality management system for the production and service of PE pipe fittings and PE ball valves; issued by Zhongjing Certification.

ISO 14001:2015 - environmental management system
Environmental management system for the production and service of PE pipe fittings and PE ball valves; issued by China Economic Certification.

ISO 45001:2018 - occupational health and safety
Occupational health and safety management system for production and service activities; issued by Zhongjing Certification.

WRAS material approval
UK approval for material in contact with drinking water: PE100 black HDPE fittings to BS 6920-1:2014, for water up to 65 °C.

GB/T 27922-2011 - five-star after-sales service
After-sales service system of the HDPE pipe fittings range evaluated to the GB/T 27922-2011 commodity after-sales service standard at five-star level.
Dispatch, caps and thread protection
Threads are the part of this fitting that travels worst. Every threaded end ships with a protective cap or plug over the thread, and the PE socket keeps its own cap so the fusion surface is clean when the box is opened. A transition fitting for a gas meter is packed in its own carton with the thread size printed on the outside, so the fitter does not have to open every box in the consignment to find the right one.

Finished PE fittings warehoused and staged for shipment at the Qingfa works
Before you order a threaded transition
What is the price per piece?
Price depends on size, thread and quantity. We are the manufacturer, so we quote against your actual list rather than from a catalogue - send the size and thread combination and the quantity.
Are these suitable for gas as well as water?
The PE100 material is used for both. Confirm the intended medium on enquiry so the correct certificate range is quoted with the offer. A transition fitting for a gas meter and one for a water service are built to the same geometry, but the certificate cited on the paperwork differs.
Can I get a sample before placing the order?
Yes. Send the thread and PE size you need and we will arrange a sample for trial make-up on your meter union. Buyers who have previously used a steel plastic adapter PE type from another supplier usually ask for a sample first, because the thread engagement is the part that has to match.
What is the lead time?
The dn25 to dn63 threaded range is a stock item in the most common thread pairings. Unusual combinations of PE steel transition fittings are made to order; we confirm the date in the quotation.
Do you make a version for a specific national thread standard?
Tell us the standard the connection has to meet and we will confirm whether the thread is available or whether the part has to be made to order.
Hot Tags: ductile iron threaded steel to plastic transition fitting, China ductile iron threaded steel to plastic transition fitting manufacturers, suppliers, factory
You Might Also Like


Send Inquiry